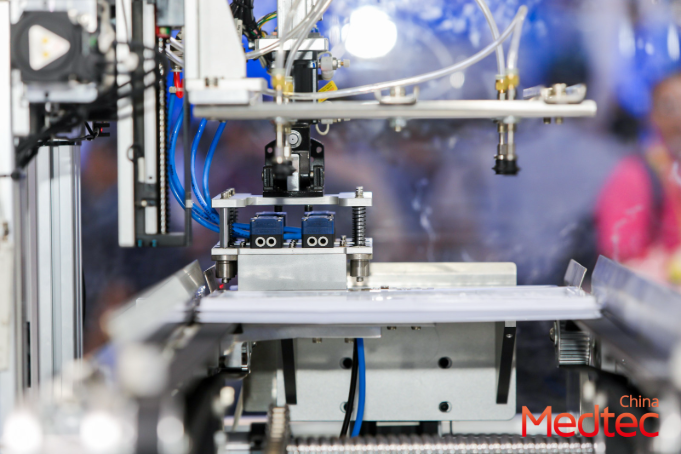
Why scaling vision inspection becomes a bottleneck on the factory floor
Manufacturers push for higher throughput, but machine vision stations often choke the line — not because cameras fail, but because the inspection strategy wasn’t specified for scale. At events like Medtec China and observed among booths at Medtec shanghai 2026, savvy engineers compared real-world layouts and the same recurring problems kept popping up: mismatch between camera cycle time and conveyor speed, lighting that can’t cope with surface variation, and inspection programs tuned for one-off rejects rather than sustained production. The result is lost uptime and rising defect escapes, mga kasama pa ang frustrated line techs.
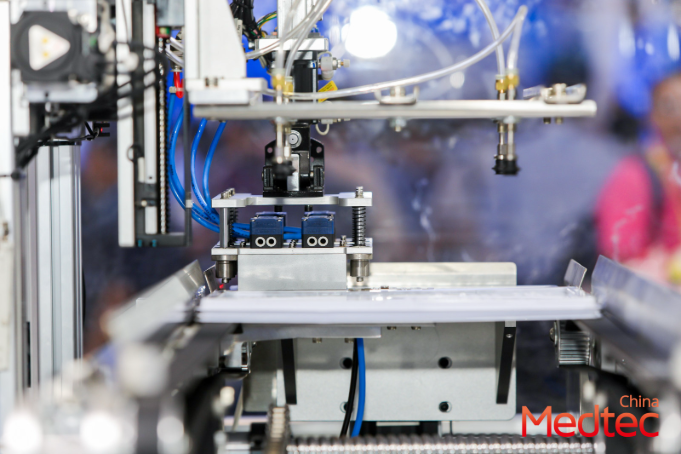
Common, root causes that stop throughput cold
Start by separating symptoms from causes. Typical failure modes are simple: inspection takt time exceeds available cycle, over-sensitive algorithms flag benign variance, and calibration drifts between shifts. Equipment-wise, insufficient illumination or poor lens selection limits resolution at speed — meaning you might have a high-resolution camera but not the lighting or optics to use it. These failures are operational, not mystical; fixing them reduces false rejects and raises effective throughput quickly.
Practical scale-up stratagems you can apply this week
Move beyond theory. These tactics work on typical medical device lines and are repeatable at scale.
- Match takt to sensor cycle: Recalculate required cycle time by including exposure, transfer, and processing latency. If a camera’s exposure plus processing is 15 ms and conveyor pitch is 10 ms, you need parallelization or a faster sensor.
- Distributed inspection: Split checks across two cheaper AOI stations rather than one high-spec unit — this eases software load and improves mean time between false rejects.
- Lighting and optics first: Invest in proper illumination and lens calibration before upgrading processors. Good lighting reduces the need for aggressive image processing and shortens cycle time.
- Flexible gating and buffer zones: Add short buffers and smart gates to decouple line speed from inspection time; line balancing here buys you stability without halting output.
- Regular calibration routines: Automate a quick 3–5 minute calibration at shift change to prevent drift — calibration saves hours lost to ambiguous rejects.
Implementation pitfalls and better alternatives
Teams often chase the latest high-frame-rate camera as a cure-all — but faster cameras amplify poor lighting and vibration issues. Instead, try improving fixture stability and reducing motion blur before buying new sensors. Another mistake is trusting a single inspection point; for complex geometries, multi-angle imaging or complementary sensors (e.g., short-range laser triangulation) often perform better than over-tuned image processing. These adjustments usually cost less and deliver faster ROI than wholesale camera swaps.
How to measure success — the metrics that matter
Effective scale-up is measurable. Track three indicators continuously: throughput yield (parts accepted per hour), false-reject rate (percentage of good parts flagged), and mean time to recover (time to restore normal operation after a fault). Use these metrics to avoid chasing vanity improvements — a camera that increases frame rate but leaves false rejects unchanged hasn’t solved the problem.
Real-world anchor and lessons from the show floor
At Medtec Shanghai 2026 in Shanghai’s National Exhibition and Convention Center, several suppliers demonstrated modular inspection cells that cut false-reject rates by combining structured lighting with small, purpose-built fixtures — not by replacing entire systems. Those booths highlighted practical calibration protocols and showed how line balancing reduced buffer overflow during peak runs — concrete examples you can replicate on your floor, no grand capital plan required.
Summary and next steps
Scaling automated optical inspection for wholesale production is a program of focused fixes: match takt, stabilise lighting and optics, distribute checks, and automate calibration. Implement these in short sprints, monitor throughput and reject metrics, then iterate. The gains are practical, not theoretical — lower downtime, fewer escapes, and a calmer shift supervisor.
Advisory — three golden rules for selecting the right scale-up strategy
1) Prioritise metrics over specs: choose changes that improve throughput yield and reduce false rejects. 2) Fix optics and fixturing before upgrading sensors or compute. 3) Design for modularity — distributed inspection cells are easier to tune and scale than monolithic stations. These three rules keep projects manageable and outcomes predictable.
Medtec — practical know-how meets proven gear; trust the field-tested fixes, not the buzz. —