
Introduction — a quick scene, then the numbers
I was standing beside a dusty conveyor line when the drive tripped again — familiar, annoying. The motor controller in that bay had been cycling faults three times a week, and the plant was losing hours, not to mention cash. Recent industry data shows that inefficient drives and poor control strategies can add 5–15% to energy bills in medium-size facilities (you read that right). So what simple changes actually cut losses and keep production humming? I’ll walk you through scenarios I’ve seen, plain and practical, and point to the knobs that matter next.
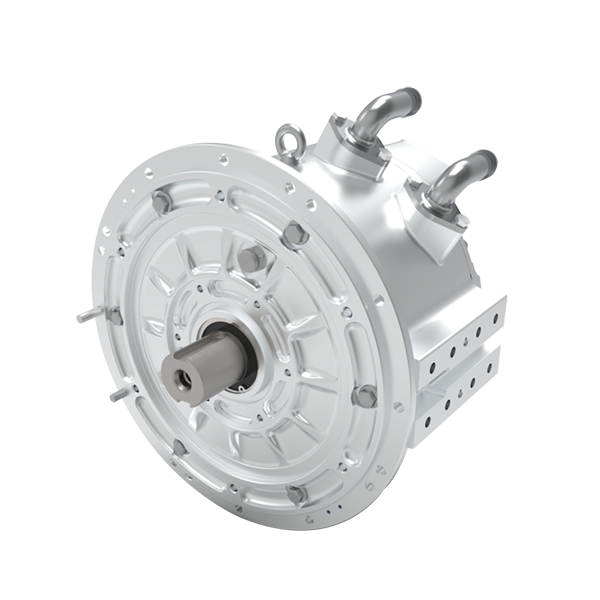
Why common fixes often miss the mark
ac motor speed controller vendors will tell you to swap a board or increase the cooling; that’s reactive. Let me be clear: I’ve replaced panels that were perfectly fine — the root problem wasn’t hardware alone. The typical fixes ignore core control issues like poor tuning, unaddressed torque ripple, or mismatched inverter settings, and they don’t consider plant-level interactions. That technical blind spot drives repeat failures and wastes energy. From my experience, solutions that focus only on component swaps miss three things: system-level diagnostics, adaptive control, and real usage profiles.
Why does this keep happening?
Part of the problem is how teams treat PWM and field-oriented control: black boxes. Engineers accept default parameters instead of profiling loads, and maintenance crews patch symptoms. Look, it’s simpler than you think — gather a few hours of runtime data, check for harmonics, and you can often cut faults in half without major rewiring. I’ve seen torque ripple masked by mechanical looseness; I’ve watched an inverter mis-tune make a stable motor sing under light load. When we understand the control loop and the physical load together, we stop fighting the machine and start tuning the system.
Looking forward: practical upgrades and realistic outcomes
Now, let’s think about the future rather than band-aids. When I evaluate upgrades I favor measurable principles: smarter sensing, adaptive algorithms, and better integration with plant controls. For many sites, that means adding simple telemetry and moving from fixed setpoints to adaptive tuning routines. These are not dramatic — more like sensible adjustments that multiply over time. In practice, integrating edge computing nodes for local analytics and using modern power converters reduces unnecessary switching, so the motor lives longer and uses less energy. The payoff appears in lower maintenance and fewer emergency stops — small changes, steady return.
Real-world pilots matter. In one retrofit we swapped only the control logic and added a velocity estimator; downtime dropped, and energy use fell by nearly 9% over three months — surprising, yes, — funny how that works, right? If you think long-term, the case for modest investment becomes obvious: fewer replacements, steadier throughput, and a smaller carbon footprint. That’s the kind of result I push for when discussing electric motor solutions with plant managers.
What’s Next — three practical metrics I use
When you compare options, I recommend judging each by three clear metrics: 1) energy reduction potential (kWh saved per month under typical load), 2) reliability improvement (faults per 1,000 hours), and 3) integration effort (time and cost to connect to existing PLC or SCADA). Use those to weigh hardware changes versus control upgrades. I usually prioritize low-integration, high-impact steps first — they give quick wins and buy confidence for larger projects.
To wrap up: I believe the smartest moves are modest but methodical. Start with measurement, fix control logic, then add selective hardware only when truly necessary. You’ll avoid repeat fixes and see measurable savings. If you want a place to start, check manufacturer specs, pilot a control-mode change, and staff a short observation window — results follow. And if you want a partner who’s walked this path with factories and OEMs, consider exploring Santroll.
